- This topic is empty.
-
AuthorPosts
-
2026-11-11 at 5:31 pm #13029
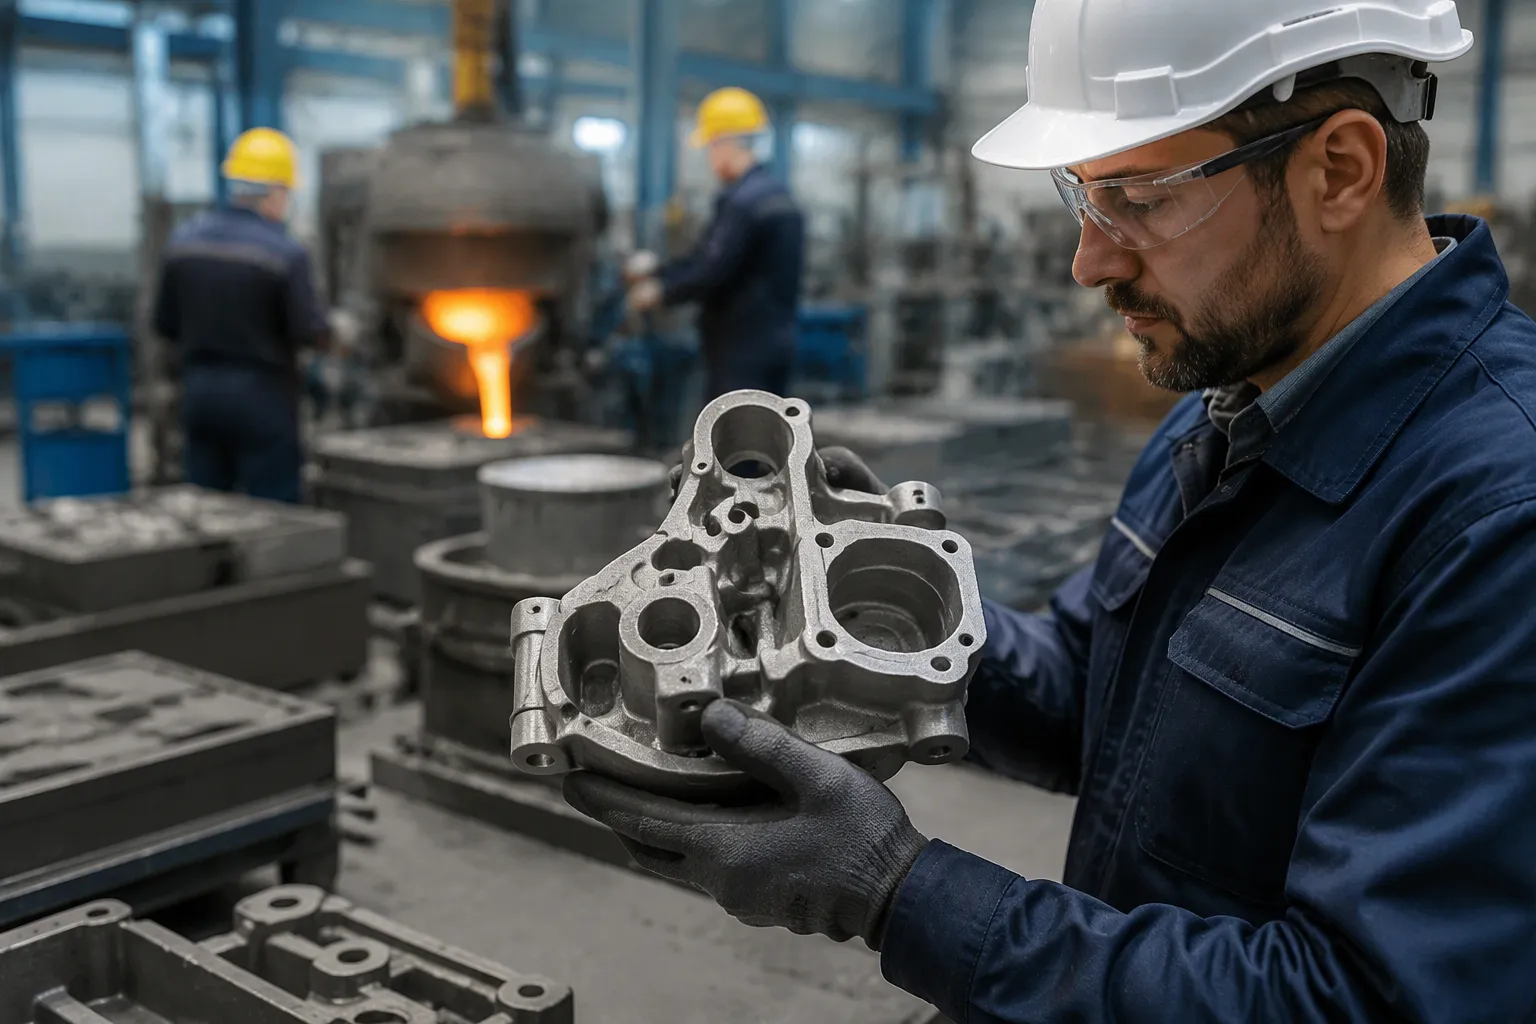
Image Source: https://www.xuxiangtaimetal.com Custom alloy casting produces parts from a specified alloy and part design. Each component matches an OEM’s form, fit, and function requirements. This approach gives manufacturers design freedom, consolidated part counts, application-matched material performance, and repeatable production volumes. A systematic, stage-by-stage process reduces rework, cost surprises, and timeline risk.
Key Takeaways
- Custom alloy casting gives OEMs design freedom and reduces part counts.
- Early design review with the caster prevents costly problems later.
- A step-by-step process protects your budget and schedule.
Write a Professional Article About Custom Alloy Casting: What It Is and Why OEMs Use It
Definition and Scope
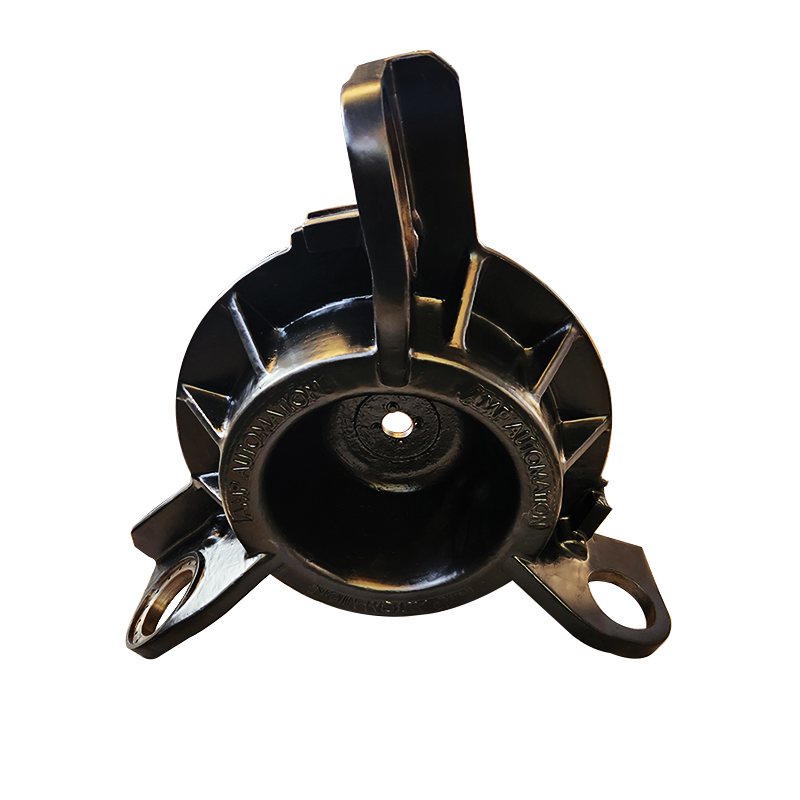
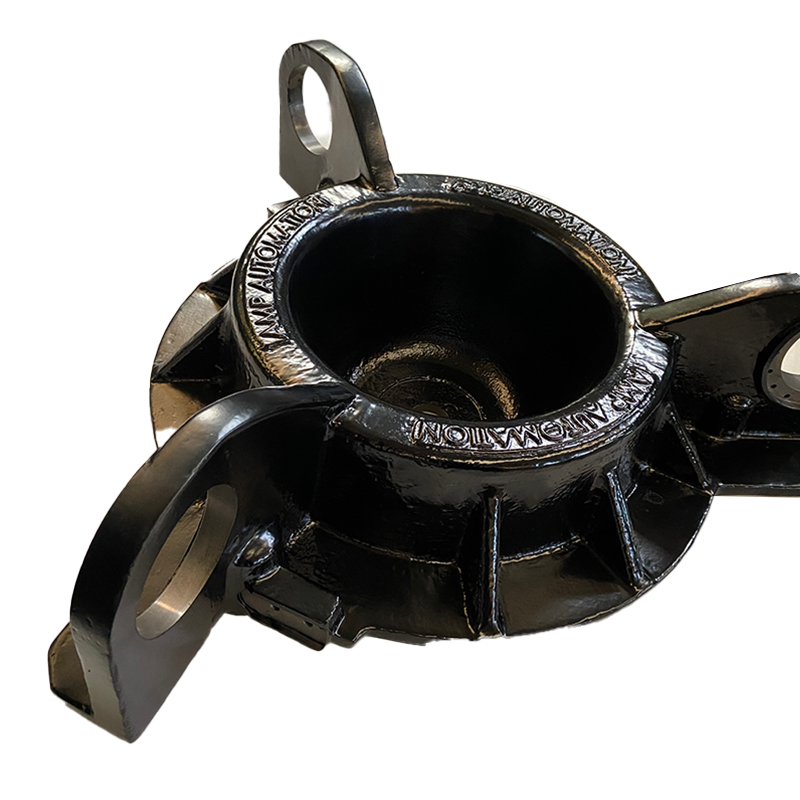
Custom alloy casting is a manufacturing process that produces metal components from a specified alloy and a customer-supplied part design. The scope covers the full chain: alloy selection, pattern and mold development, melting and pouring, and secondary CNC finishing. Each step aligns with the OEM’s form, fit, and function requirements. The process suits irregular cavities, multi-lug shapes, and variable-thickness structures. One molding cycle forms an integrated part. This approach replaces welded assemblies and solid bar machining for complex industrial components.
How It Differs from Standard Casting
Standard casting relies on fixed patterns and catalog alloys. Custom alloy casting starts from the OEM’s drawing or STEP file. The caster designs the process, develops the mold, and controls defects for that specific part. Alloy chemistry, tolerances, and inspection criteria follow the application. Standard casting offers limited design input. Custom casting delivers a tailored part with documented material and dimensional records.
Where OEMs Benefit Most
OEMs gain the most in heavy-duty industrial machinery, air compressors, and fluid equipment. Complex housings, pump and valve bodies, and compressor spare parts often need one-piece structures. Custom casting forms these shapes in a single molding step. The result is better structural integrity than welded assemblies and lower material waste than direct CNC machining. Prototype trial production and mass production both run on the same process design. This consistency protects repeatable production volumes.
Design Considerations and DFM
Image Source: https://www.xuxiangtaimetal.com Wall Thickness and Geometry Rules
Uniform wall thickness supports clean metal flow and even cooling. Thin sections cool fast and may not fill completely. Thick sections cool slowly and can form shrinkage porosity. Designers should keep walls as consistent as the process allows and blend transitions gradually. Casting forms irregular cavities, multi-lug shapes, and variable-thickness structures in one molding cycle, so geometry rules matter from the first sketch.
Draft, Radii, and Tolerances
Draft angles let the pattern release from the mold without tearing sand or damaging the cavity. Sharp internal corners concentrate stress and restrict metal flow. Added radii improve both. Tolerances should reflect the process capability, not an arbitrary default. A caster confirms achievable tolerances during review, and the OEM then sets critical dimensions with machining in mind.
Machining Allowance
Cast surfaces rarely serve as final mating surfaces. The designer adds stock to faces that will be milled, turned, drilled, or tapped. Allowance depends on part size, alloy, and fixture strategy. Too little stock leaves defects on the finished surface. Too much stock wastes material and cycle time. The caster and machinist agree on allowance values before tooling begins.
Early DFM Review with the Caster
An early DFM review catches costly geometry issues before mold development starts.
The caster reviews the drawing or STEP file for wall transitions, draft, radii, and machining stock. Feedback at this stage protects the tooling investment and shortens the path to first articles.
Choosing the Right Alloy
Technical Performance Factors
Alloy selection starts with mechanical requirements. Tensile strength, hardness, fatigue resistance, and elongation define the performance envelope. Thermal conductivity and wear resistance matter for compressor spare parts and pump and valve components. The engineering team matches alloy chemistry to the load case and duty cycle. Castability also counts. Some alloys flow well and resist hot tearing. Others demand tighter process control during pouring and cooling.
Application Fit and Environment
The service environment shapes the alloy decision. Fluid equipment demands corrosion resistance against the pumped medium. Air compressor parts face heat and pressure cycling. Industrial machinery housings carry vibration and shock loads. Designers should document temperature range, chemical exposure, and load profile before the first DFM review. This information guides the caster toward an alloy that performs across the full service life.
Standards Compliance
OEMs often specify recognized standards for chemistry and mechanical properties. Common references include ASTM, ISO, and EN grades for aluminum and gray iron. The caster verifies conformance through material test records and inspection reports. Export shipments require documentation that supports traceability. Compliance checks belong in the quoting stage, not after tooling starts.
Cost and Availability Trade-offs
Alloy price and lead time vary with market supply. A premium grade may deliver longer service life and lower total cost. A standard grade may suit non-critical housings and protect budget. The caster reviews both options with the OEM and documents the trade-off. Early agreement on alloy grade prevents cost surprises during mass production.
Selecting a Casting Process
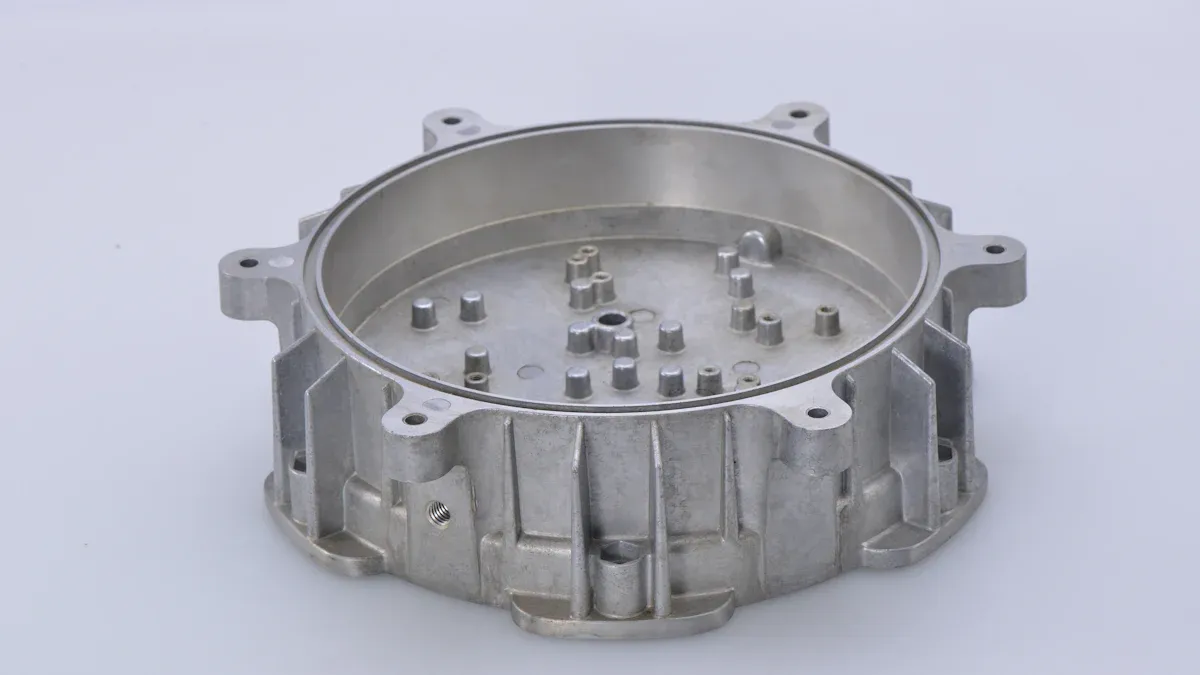
Image Source: https://www.xuxiangtaimetal.com Sand, Investment, and Die Casting Compared
Each casting process offers distinct strengths. Sand casting uses reusable patterns and handles large, heavy parts with complex internal cavities. Investment casting delivers fine surface detail and tight dimensional control for smaller, intricate components. Die casting suits high-volume production of non-ferrous parts with excellent repeatability. The table below summarizes the key differences.
Factor Sand Casting Investment Casting Die Casting Part size Large to very large Small to medium Small to medium Surface finish Moderate Excellent Excellent Dimensional tolerance Wider Tight Tightest Tooling cost Low Moderate High Best volume Low to medium Medium High Matching Process to Volume and Tolerance
Volume and tolerance requirements drive the process decision. Low-volume industrial machinery housings fit sand casting well. Precision pump and valve components with fine features favor investment casting. High-volume compressor spare parts justify die casting tooling. The engineering team reviews both factors during DFM review and recommends the process that balances cost and quality.
Tooling Implications and Lead Time
Tooling scope changes with the process. Sand casting needs patterns and core boxes. Investment casting needs wax dies and shell tooling. Die casting needs hardened steel molds. Tooling cost and lead time rise with process complexity. Early process selection protects the production schedule and avoids late redesign.
Prototyping, First Articles, and Quality Control
Prototype Methods and Fidelity
Prototyping validates the design before tooling investment grows. The method depends on part complexity, alloy, and how closely the prototype must match production. For sand casting projects, the caster can machine a pattern from a CAD model and pour a trial part in the specified alloy. This route delivers high fidelity to the final production process. The prototype shares the same alloy chemistry, solidification behavior, and defect profile as the mass production run.
Investment casting prototypes often start from a printed wax pattern. The caster builds the shell and pours the alloy, then applies CNC finishing to the critical features. This method captures fine surface detail and tight tolerances early. Die casting prototypes typically use a temporary tool or a machined substitute. The OEM should confirm which features the prototype must represent and which features can wait for production tooling.
Fidelity matters most at interfaces. Mounting faces, bore diameters, and mating surfaces should match production intent. Cosmetic features and non-critical radii can tolerate looser fidelity. The engineering team reviews the prototype plan with the OEM and sets clear acceptance criteria before the first pour. Casting simulation supports this stage. The team models fill and solidification, predicts shrinkage locations, and adjusts gating before metal flows.
First Article Inspection
First article inspection (FAI) confirms that the first production part meets every drawing requirement. The process begins with a full dimensional layout. The inspector measures every dimension on the drawing, not a sample. Reports record actual values against nominal and tolerance limits. Critical features receive extra attention, including bore positions, flatness, and wall thickness at load-bearing sections.
FAI also covers material and process verification. The caster confirms alloy chemistry against the specification and reviews heat treatment records. Visual inspection checks surface condition, gate remnants, and parting line quality. Any deviation triggers a corrective action before mass production starts. The OEM signs off on the FAI report, and that signed document becomes the baseline for production acceptance. A complete FAI package protects both parties. It proves the process is capable and gives the OEM a reference for future lots.
In-Process and Final Inspection
Quality control runs through the entire production flow, not just at the end. In-process checks catch problems while correction is still cheap. The table below summarizes the typical inspection stages for custom alloy casting.
Stage What Inspectors Check Purpose Pattern and mold Dimensions, surface condition, draft Confirm tooling readiness Melt and pour Chemistry, temperature, inoculation Control alloy quality Post-cast cleaning Visual defects, gate removal Catch surface and fill issues CNC finishing Critical dimensions, feature positions Verify assembly fit Final inspection Full dimensional and visual review Release the lot In-process inspection at the melt stage verifies chemistry before pouring. Spectrometer readings confirm the alloy matches the specification. Pouring temperature and mold condition receive checks against the process sheet. After cleaning, inspectors look for shrinkage, porosity, cracks, and cold shuts. These defects are easier to isolate before machining adds cost.
Final inspection confirms the finished component meets all drawing requirements. The inspector reviews dimensions, surface finish, and marking. Sampling plans follow the OEM’s requirements or an agreed standard. Any nonconformance goes to a material review board. The board decides on rework, concession, or scrap. Documented decisions keep the production record complete.
NDT and Material Verification
Non-destructive testing (NDT) finds internal defects without cutting the part. Common methods include radiographic testing, ultrasonic testing, dye penetrant inspection, and magnetic particle inspection. Radiography reveals internal porosity and shrinkage in thick sections. Ultrasonic testing detects subsurface discontinuities in heavier castings. Dye penetrant inspection exposes surface-breaking defects on non-porous surfaces. Magnetic particle inspection suits ferromagnetic alloys such as gray iron.
The OEM and caster agree on NDT methods, coverage, and acceptance criteria during the quoting stage. Critical pressure-retaining parts for fluid equipment often require full radiography of specified zones. Structural housings may need spot checks at high-stress locations. Material verification complements NDT. Tensile tests, hardness tests, and chemistry analysis confirm the alloy meets the specified grade. Test bars are cast with the production lot and traceable to that lot. The engineering team reviews results against the standard before release.
Documentation and Traceability
Documentation turns a good part into a verifiable part. The production record follows the component from melt to shipment. It includes heat numbers, chemistry results, inspection reports, and material test records. Each lot carries a unique identifier. That identifier links the finished part back to its casting date, alloy batch, and inspection results.
Traceability supports export shipments. Certificates of Origin, customs declarations, and compliant packaging documentation travel with the goods. If a question arises months later, the OEM can pull the record and confirm the part’s history. The caster provides production records, inspection reports, and material test records as required. This documentation practice protects the OEM’s reputation and simplifies audits. A complete record also supports continuous improvement. The team reviews past inspection data, spots recurring defect patterns, and adjusts the process before problems reach the customer.
Machining and Finishing
Machining Allowances and Fixturing
Cast blanks need CNC finishing to reach assembly-ready dimensions. The designer adds stock to faces that will be milled, turned, drilled, or tapped. Allowance values depend on part size, alloy, and fixture strategy. The caster and machinist agree on these values before tooling begins. Fixturing holds the cast blank stable during cutting. Cast surfaces vary more than machined bar stock, so fixtures must accommodate that variation. The engineering team reviews fixture design alongside the machining plan. Proper fixturing protects critical features and keeps cycle times predictable.
Surface Finishing Options
Surface finishing improves appearance, corrosion resistance, and wear performance. The table below summarizes common options for custom cast components.
Finish Best For Effect Shot blasting General cleanup Removes scale and improves surface uniformity Painting Housings and frames Adds corrosion protection and color Powder coating Industrial machinery parts Delivers durable, uniform coverage Machined finish Mating surfaces Provides precise flatness and fit The OEM selects a finish based on the service environment and cosmetic requirements. The caster confirms the finish schedule during quoting.
Heat Treatment and Post-Processing
Heat treatment relieves internal stress and adjusts mechanical properties. Stress relief after casting reduces distortion during machining. Solution treatment and aging strengthen aluminum alloy castings. Gray iron castings may receive annealing to improve machinability. Post-processing steps follow a defined sequence. Shot blasting often precedes heat treatment, and machining follows stress relief. The engineering team documents the full sequence in the process sheet. Each step receives verification through inspection records. This discipline keeps the finished component consistent across production lots.
Supplier Selection and Quoting
Capability and Certification Checks
A capable casting supplier matches process scope to the part. The OEM should confirm the supplier handles the required alloy, part size, and tolerance band. Sand casting, precision investment casting, and secondary CNC finishing should all sit under one roof or a managed chain. Certification checks cover quality management systems and material test records. The supplier should provide production records, inspection reports, and material test records on request. Export experience matters too. Compliant packaging, Certificates of Origin, and customs declarations protect international shipments.
Reading a Casting Quote
A casting quote contains more than a price per piece. The OEM should read each line for tooling cost, piece price, machining charges, and finishing steps. Quotes should state alloy grade, process, tolerance assumptions, and inspection scope. Volume breaks reveal how piece price shifts with order quantity. Payment terms, lead time, and shipping terms belong in the same document. A clear quote separates one-time tooling from recurring production cost. This structure lets the OEM compare suppliers on equal footing.
Tooling Ownership and Terms
Tooling ownership deserves a written agreement. The OEM typically pays for patterns, dies, or molds, so the contract should state who owns them. Terms should cover storage, maintenance, and transfer conditions. The agreement should also address tooling life and replacement responsibility. Clear terms protect the OEM’s investment across production runs. The supplier should confirm these points during quoting, not after the purchase order.
Production Timelines and Cost Drivers
Production timelines and cost drivers determine whether a custom alloy casting project meets its budget and delivery targets. OEMs who understand both factors make better decisions at the quoting stage. They also spot schedule risk before it becomes a crisis. This section breaks down the timeline from drawing review to shipment and explains the forces that shape piece price.
Stage-by-Stage Timelines
Every custom casting project follows a sequence of stages. Each stage consumes time and depends on the one before it. The table below shows typical durations for a mid-complexity industrial component. Actual durations vary with part size, alloy, process, and supplier workload.
Stage Typical Duration Key Activities Drawing review and DFM 3–10 business days Geometry review, tolerance check, alloy confirmation Quoting and award 5–15 business days Cost build, terms negotiation, purchase order Tooling and pattern development 2–6 weeks Pattern fabrication, core boxes, die or mold build Casting simulation 3–7 business days Fill and solidification modeling, gating adjustment First pour and prototype 1–3 weeks Trial casting, rough inspection, dimensional check First article inspection 1–2 weeks Full layout, material testing, OEM sign-off Production casting 2–6 weeks Melting, pouring, cleaning, lot inspection CNC finishing 1–3 weeks Milling, turning, drilling, tapping, final inspection Surface finishing and packing 3–10 business days Shot blasting, coating, export packaging Shipping and documentation 1–4 weeks Freight booking, Certificates of Origin, customs The total timeline for a new part often runs 10 to 20 weeks from drawing to delivery. Repeat orders skip tooling and first article stages, so they move much faster. A repeat production run may complete in 4 to 8 weeks. OEMs should plan the first order with the full timeline in mind and treat later orders as a shorter cycle.
Tooling sits on the critical path for most new projects. Pattern fabrication and mold development cannot compress easily without adding cost. The engineering team can run casting simulation in parallel with tooling work. This overlap saves days without sacrificing quality. Early DFM review also shortens the path. Issues caught at drawing review cost hours to fix. Issues caught after the first pour cost weeks.
Key Cost Drivers
Piece price reflects several cost drivers. Each one responds to design and sourcing decisions. OEMs who understand these drivers negotiate from a stronger position.
Tooling cost is a one-time charge. Patterns, core boxes, wax dies, and steel molds carry different price tags. Sand casting tooling costs less than die casting tooling. The OEM pays this cost once and amortizes it across production volume. Higher volume spreads tooling cost thinner per part.
Material cost tracks alloy grade and market price. Aluminum and gray iron prices move with supply conditions. A premium alloy raises piece price. The caster should state the alloy grade and the pricing basis in the quote. Some quotes tie material cost to a published index. This practice protects both parties from market swings.
Labor and machine time drive conversion cost. Complex geometry needs more molding time and more finishing passes. Tight tolerances add inspection time. Multi-lug shapes and irregular cavities raise the labor content per part. The caster estimates these hours during quoting and builds them into piece price.
Machining cost depends on stock allowance and feature count. Every milled face, drilled hole, and tapped thread adds cycle time. Designers who specify generous tolerances on non-critical features reduce machining cost. Critical interfaces still need precision, but cosmetic surfaces rarely do.
Inspection and documentation add cost at the high end of the quality scale. Full radiography, tensile testing, and lot traceability carry real charges. The OEM should match inspection scope to part criticality. A pressure-retaining valve body justifies full NDT. A non-structural cover plate does not.
Order quantity shapes unit cost across every driver. Setup time, tooling amortization, and material purchasing all favor larger lots. Small prototype runs carry a higher unit price by nature. The quote should show volume breaks so the OEM sees the cost curve.
Early decisions in design, alloy, and process have the largest downstream impact on cost and quality.
A design change after tooling starts can wipe out the savings from a lower quote. The cheapest path runs through thorough DFM review before the purchase order.
Managing Schedule Risk
Schedule risk comes from several directions. Tooling delays, material shortages, inspection failures, and shipping disruptions all threaten delivery dates. A systematic approach reduces exposure to each one.
Buffer time belongs in the plan from day one. The OEM should build contingency into the master schedule, not assume every stage finishes on its fastest day. A two-week buffer before a critical assembly date absorbs most routine delays. The caster should confirm realistic lead times during quoting and flag any stage with tight capacity.
Early supplier communication protects the schedule. The OEM should share the target delivery date and the consequences of a slip. The caster can then sequence work to protect that date. Regular status updates at each stage give the OEM visibility. A weekly check on tooling progress and casting status catches problems while correction is still possible.
Parallel work streams compress the timeline. Casting simulation can run alongside tooling fabrication. Prototype machining can start as soon as the first casting passes rough inspection. Documentation preparation can proceed during production. The engineering team plans these overlaps during project kickoff.
Risk also lives in the design itself. A part with marginal draft or thin walls may fail first article inspection. Rework then pushes the schedule. Early DFM review removes this risk before tooling begins. The same logic applies to alloy choice. An alloy with poor castability may generate high scrap rates and unpredictable delivery. The caster should confirm alloy castability during the quoting stage.
Clear acceptance criteria prevent late disputes. The OEM and caster should agree on inspection scope, sampling plans, and acceptance standards before the first pour. A signed first article report becomes the production baseline. Later lots then move through inspection without debate. This clarity protects the delivery schedule across the full production run.
Export shipments add their own risk layer. Customs clearance, freight capacity, and documentation errors can delay delivery. The caster should prepare Certificates of Origin and customs declarations early. Compliant packaging protects parts in transit. The OEM should confirm shipping terms and Incoterms in the quote. A documented logistics plan removes surprises at the port.
A repeatable system ties all these practices together. DFM review, prototyping, quality control, and clear supplier communication form one workflow. OEMs who run this workflow on every project protect their timelines and their production outcomes. The same discipline that controls cost also controls schedule. Both depend on decisions made early and verified at each stage.
Custom alloy casting follows a repeatable system. The workflow runs from design and DFM review through alloy selection, process choice, prototyping, and quality control. Early decisions in design, alloy, and process carry the largest downstream impact on cost and quality. A systematic approach protects timelines and production outcomes.
FAQ
How long does a custom alloy casting project take from drawing to delivery?
A new part typically runs 10 to 20 weeks. Repeat orders skip tooling and first article stages, so they complete in 4 to 8 weeks.
What minimum order quantity does a custom casting supplier accept?
Suppliers support prototype trial production and mass production. Minimum quantities vary by process and tooling. The caster confirms acceptable lot sizes during quoting.
Which documents accompany an export shipment of custom cast components?
The caster provides production records, inspection reports, and material test records. Certificates of Origin and customs declarations travel with compliant export packaging.
See Also
Avoid Picking The Incorrect Aluminum Casting Method Ever Again
https://www.xuxiangtaimetal.com
Qingdao Xuxiangtai Machinery -
AuthorPosts

- You must be logged in to reply to this topic.