- This topic is empty.
-
AuthorPosts
-
2026-11-11 at 5:37 pm #13036
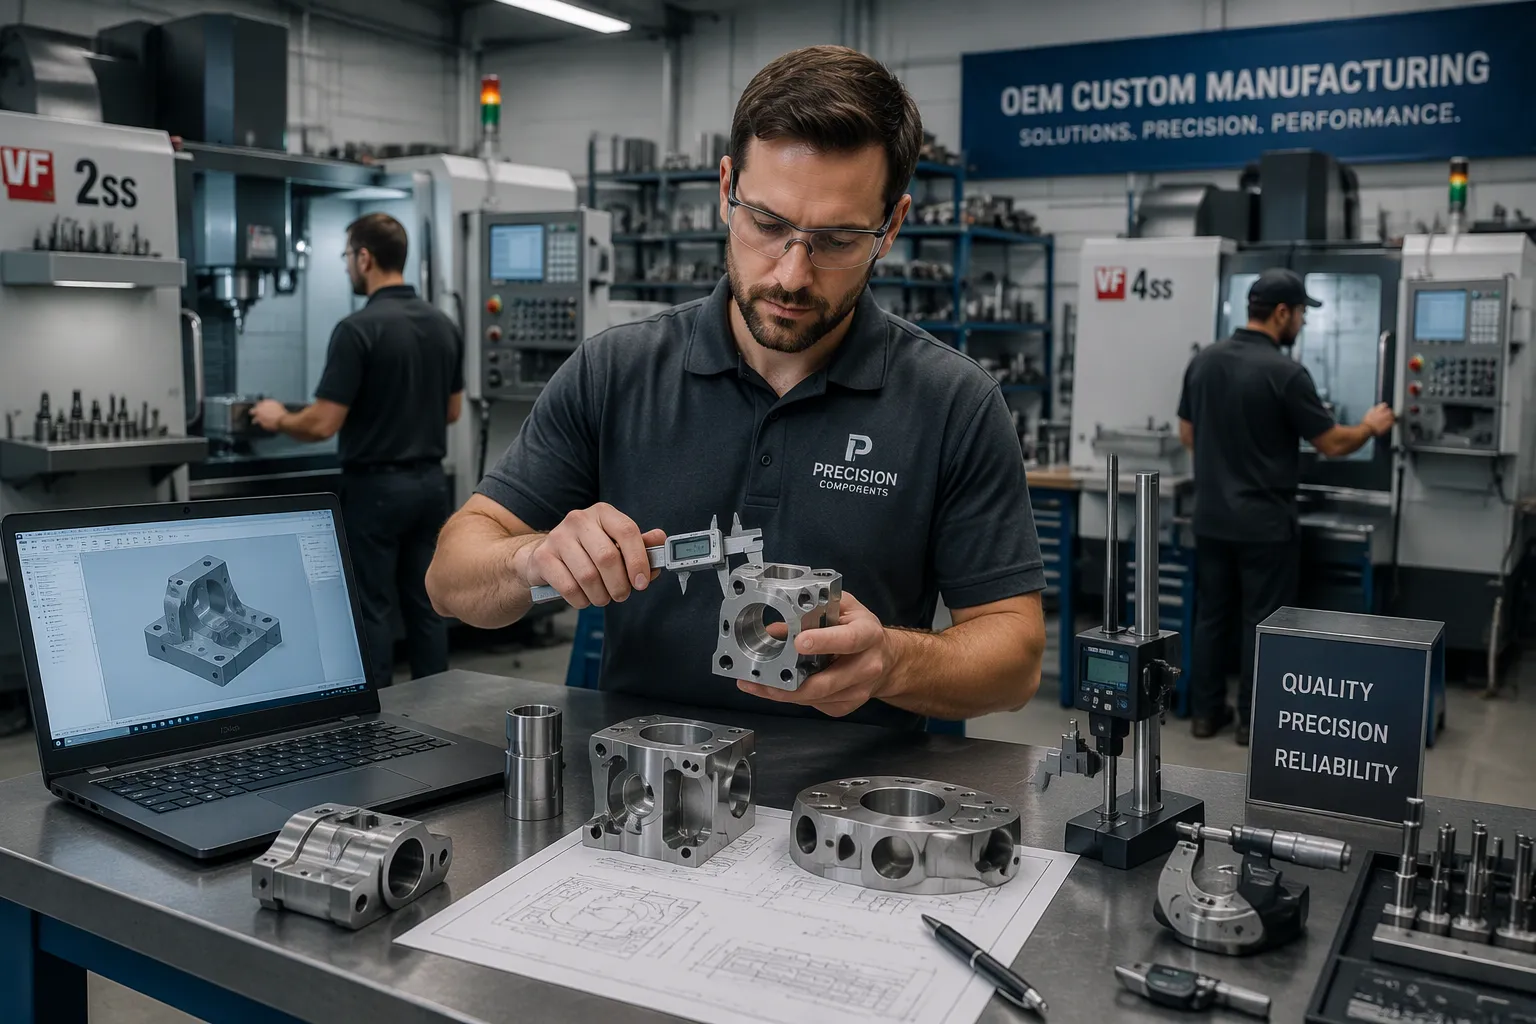
Image Source: https://www.xuxiangtaimetal.com Qingdao Xuxiangtai Machinery Manufacturing Co. turns customer drawings, samples, material specs, and technical documents into finished metal components that meet 2026 OEM specifications. Write a professional brand article about the metal component manufacturing business of Qingdao Xuxiangtai Machinery Manufacturing Co., and the fixed six-stage process stands out: input review, engineering and process planning, material sourcing and verification, production with in-process quality control, final inspection and documentation, and packaging and delivery. Each stage has a defined owner, a checklist, and a sign-off. Customers track and confirm requirement translation at every stage through documented reviews and approvals.
Key Takeaways
- Xuxiangtai follows a six-stage process to turn your drawings and samples into precise metal parts.
- You review and approve each stage, so you always know how your requirements are being met.
- Every shipment includes detailed inspection reports and material certificates for full traceability.
Stage 1: Receiving and Reviewing Customer Inputs
Qingdao Xuxiangtai Machinery Manufacturing Co. builds its entire custom metal component business on one principle: the finished part can only be as accurate as the input that starts it. Stage 1 exists to close that gap before any machine runs. Industrial OEM buyers rarely send a single clean file. They send a drawing package, a worn sample, a material callout, a pressure rating, and a stack of technical documents, often assembled by different engineering teams over several years. Xuxiangtai treats this mixed input as the raw material of the project and reviews it as a whole.
Common custom component requirements from industrial customers follow recognizable patterns. Automotive buyers specify tight dimensional tolerances and full traceability. Aerospace and energy customers add high-temperature alloys and complex internal geometry. Medical device manufacturers prioritize surface finish and repeatable mechanical movement. Heavy equipment builders focus on structural strength and vibration damping. Each requirement set points to a different mix of casting, machining, sheet metal fabrication, or additive manufacturing. The review team reads the input with those downstream choices in mind.
Drawing Review and Tolerance Checks
The drawing review begins with a full read of every dimension, tolerance, datum, and note on the customer’s 2D drawings and 3D models. Engineers check that the model and the drawing agree. They confirm that datums are defined in a way a machinist can actually hold. They flag tolerances that sit tighter than the process can reliably deliver, and they identify features that need special tooling, five-axis setups, or EDM work.
Tolerance checks go beyond a simple pass or fail. The team maps each critical dimension to the process that will produce it. A bore tolerance on a stainless steel housing may call for CNC turning with a composite milling operation. A flatness callout on a cast aluminum cover may require a post-casting machining step. This mapping happens at the drawing stage, not on the shop floor. Catching a tolerance conflict here saves weeks of rework later.
Geometry also enters the review. Deep pockets, thin walls, undercuts, and internal channels each raise different questions. Some geometries suit precision investment casting. Others suit five-axis milling or metal 3D printing. The review team notes where geometry pushes against a conventional process and where an additive approach removes the constraint entirely.
Sample Evaluation and Reverse Engineering
Many OEM customers send a physical sample instead of, or alongside, a drawing. The sample may be a legacy part with no surviving documentation, a competitor component the customer wants to reproduce, or a prototype that performed well in testing. Xuxiangtai evaluates each sample with measurement tools and, where needed, 3D scanning. The goal is a complete digital record of the part as it actually exists.
Reverse engineering turns that record into a manufacturable definition. Engineers capture critical dimensions, wall thicknesses, fillet radii, and surface conditions. They compare the scanned geometry against any partial drawings the customer provides. Discrepancies between the sample and the drawing get documented and raised with the customer before anyone commits to a process. A worn sample can hide years of service deformation, and the team distinguishes design intent from wear.
The sample also informs material and process decisions. A failed cast part may point toward a forging or a ductile iron substitution. A machined component with a complex internal manifold may be a strong candidate for metal 3D printing. Sample evaluation therefore feeds directly into the engineering planning that follows in Stage 2.
Material Specifications and Technical Documents
Material specifications carry the same weight as geometry in the review. Customers name grades, standards, and performance requirements in their technical documents. A typical package includes the material grade, the applicable standard, pressure rating class, surface treatment specification, and inspection requirements. Xuxiangtai’s engineers read every document and confirm that the named material is available, machinable or castable at the required quality, and compatible with the specified surface finish.
The company’s process covers a wide material range. Precision investment casting handles stainless steel, carbon steel, and alloy steels. Die casting covers aluminum and zinc. Sand casting supports QT450 ductile iron for heavy structural bases. CNC machining works across metal alloys to ultra-tight tolerances. Metal 3D printing processes titanium and nickel-based high-temperature alloys. Each material brings its own considerations for wall thickness, heat treatment, and post-processing, and the review captures those notes in the project file.
Technical documents also define the acceptance criteria. Pressure ratings at Class 150, 300, 800, and 1600, ASME B16.11 compliance, RoHS environmental requirements, and IATF 16949 quality controls all shape the inspection plan. The review team extracts these criteria and links them to the final inspection stage, so nothing gets discovered late.
The Requirement Review Checklist and Sign-Off
Every project passes through a structured requirement review checklist before it moves forward. The checklist converts the customer’s input into a controlled internal record. Each line item has an owner and a status, and the completed checklist requires a formal sign-off from engineering and quality.
Checklist Item What the Team Confirms Owner Drawing and model consistency 2D drawings match the 3D model; datums are defined Engineering Tolerance feasibility Every critical tolerance maps to a capable process Engineering Sample documentation Scan data, measured dimensions, and wear notes are recorded Quality Material specification Grade, standard, and availability are confirmed Sourcing Surface treatment Finish spec is compatible with the base material Engineering Inspection criteria Pressure class, NDT, and acceptance standards are listed Quality Open questions Every ambiguity is logged and sent to the customer Project lead No project enters engineering planning until the checklist is complete and signed. An open question stays open until the customer answers it in writing.
This sign-off step is where Xuxiangtai’s documented process earns its value. Customers receive the checklist and the list of open questions for their own review and approval. They see exactly how their requirements were interpreted before a single chip is cut. The same discipline carries into Stage 2, where engineering and process planning translate the approved requirement set into a routable manufacturing plan. International customers who want to start this process can submit their drawings, samples, and technical requirements to the Xuxiangtai team for a full Stage 1 review.
Stage 2: Engineering and Process Planning
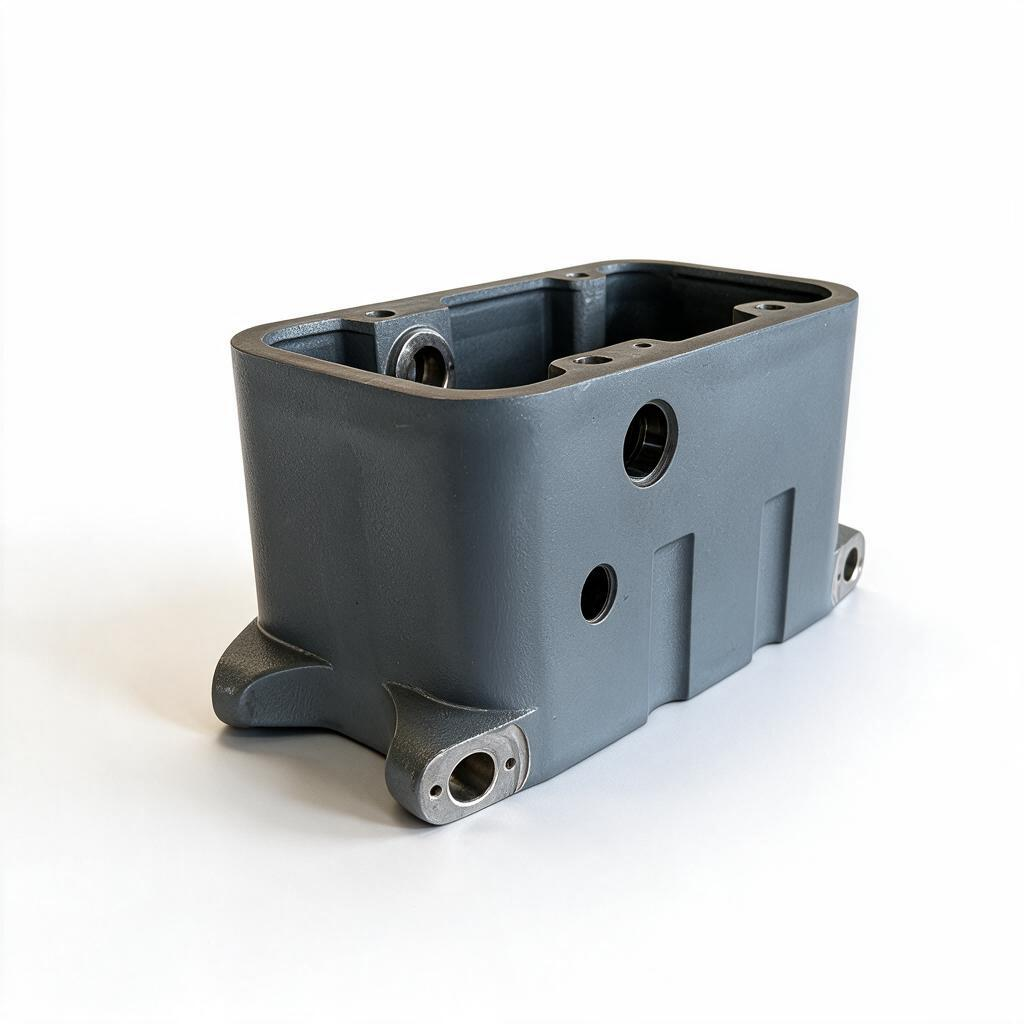
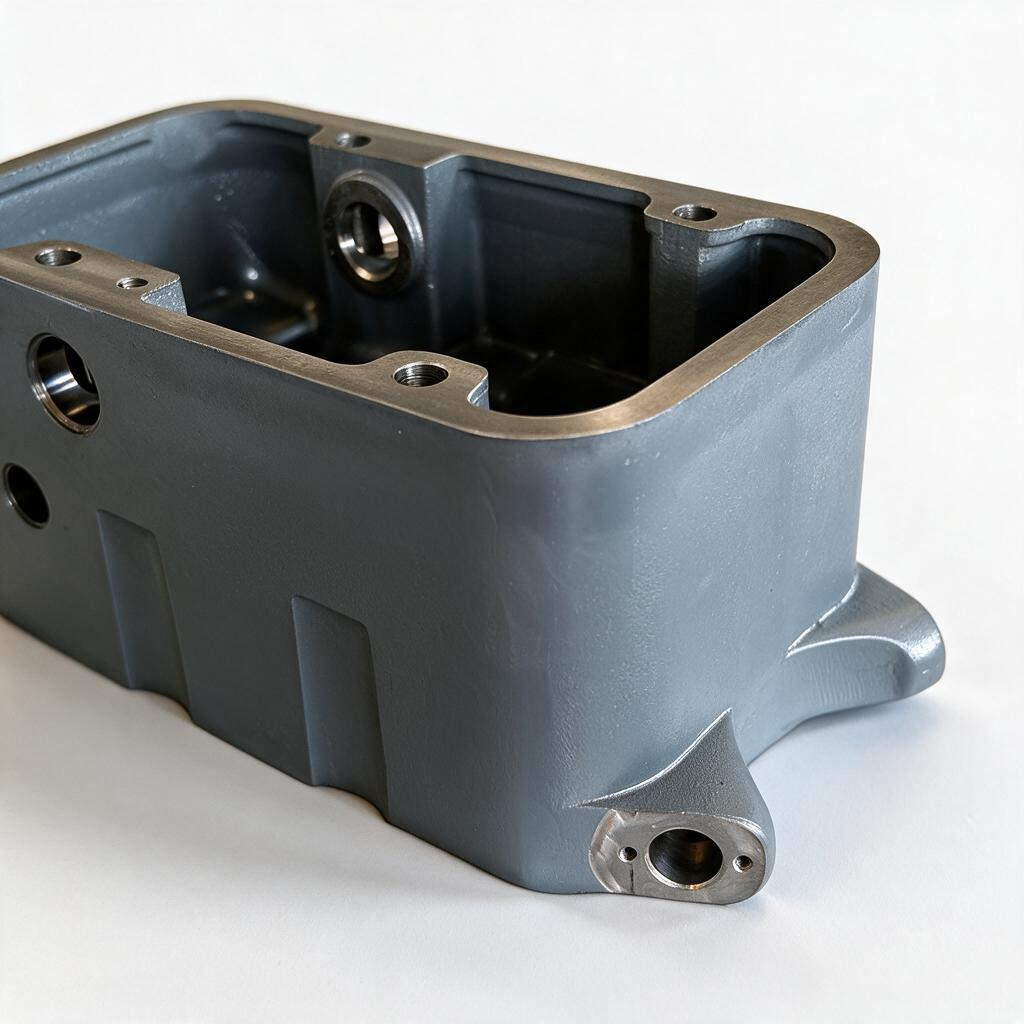
Stage 2 converts the approved requirement set into a manufacturing plan. Xuxiangtai’s engineering team owns this stage. The team turns customer intent into routable, costed, and repeatable production steps.
DFM Review and CAD/CAM Integration
The design-for-manufacturing review tests every feature against the chosen process. Engineers flag deep pockets, thin walls, and tight radii that raise cost or risk. They propose small geometry changes that protect function and improve yield. CAD/CAM integration follows the review. The team builds toolpaths and fixture concepts directly from the customer’s 3D model. This step keeps the digital definition and the shop floor plan aligned.
Process Routing Across Casting, Machining, Sheet Metal, and 3D Printing
Xuxiangtai runs four production routes under one roof. Each route fits a different part profile.
Route Best Fit Typical Strength Precision investment casting Complex steel and stainless parts Tight tolerances from the mold CNC machining Ultra-tight tolerance components Dimensional fidelity to CAD Sheet metal fabrication Enclosures and structural frames Precise bending and welding Metal 3D printing Internal channels and topological shapes Weight optimization The routing decision weighs geometry, volume, material, and pressure class. Many parts combine routes, such as a casting followed by CNC finishing.
Customer Approval Before Production
Engineering issues a process plan, a routing sheet, and a DFM report for customer review. The customer approves the plan in writing. Production starts only after this sign-off. International OEM buyers can submit drawings, samples, and technical requirements to the Xuxiangtai team to begin this planning stage.
Stage 3: Material Sourcing and Verification
Stage 3 secures the physical material that will become the customer’s part. The sourcing team owns this stage. Every purchase order traces back to a line item on the approved Stage 1 checklist.
Sourcing Materials Named in Customer Specifications
Xuxiangtai sources the exact grade the customer names. Stainless steel, carbon steel, alloy steel, aluminum, zinc, QT450 ductile iron, titanium, and nickel-based alloys all move through the same controlled channel. Approved suppliers deliver mill certificates with each lot. The sourcing team matches the certificate against the customer’s specification before the material enters the plant. A mismatch stops the order. Substitution requires written customer approval, and the team documents that approval in the project file.
Spectral Analysis and Material Validation Reports
Incoming material passes spectral analysis before release to production. The spectrometer reads the alloy composition and compares the result to the specified grade. This check catches mixed lots, mislabeled stock, and counterfeit material at the door. The quality team then issues a material validation report for the customer.
Report Element What It Confirms Alloy composition Chemistry matches the named grade Mill certificate Supplier lot and heat number are traceable Standard compliance RoHS and applicable pressure class requirements are met Release signature Quality approves the lot for production No material reaches the shop floor without a released validation report.
Customers receive these reports as part of the final documentation package. The records tie every finished component back to a verified heat of material.
Stage 4: Production and In-Process Quality Control
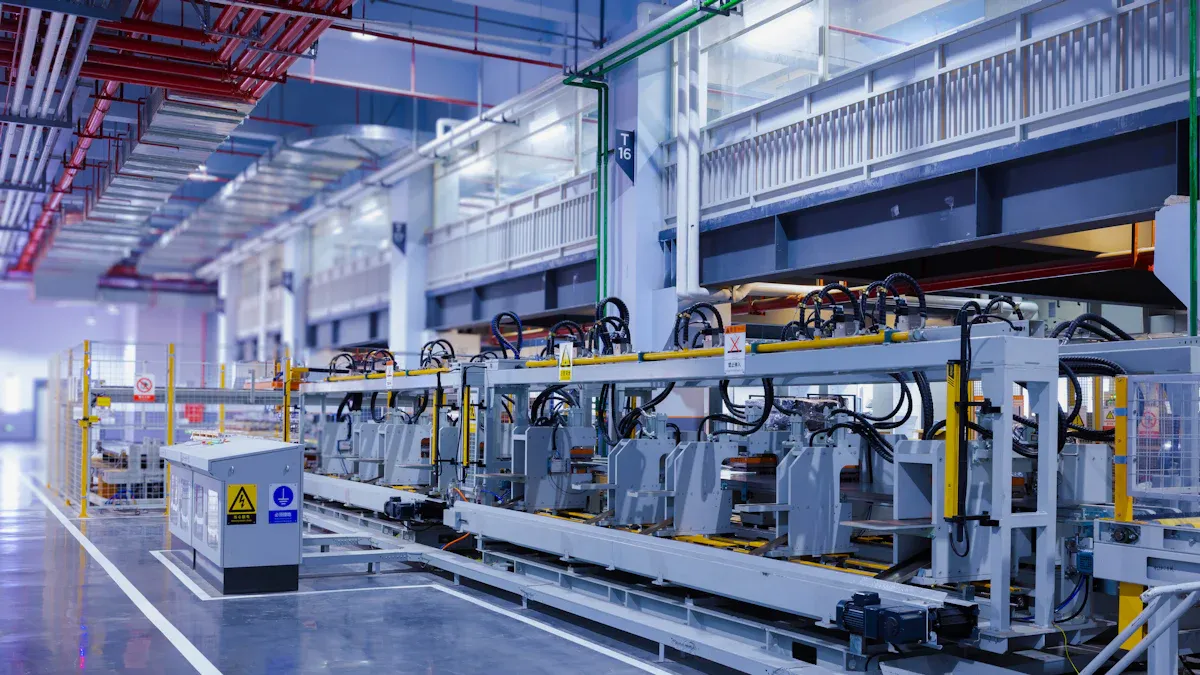
Image Source: https://www.xuxiangtaimetal.com Stage 4 is where the approved plan becomes metal. Qingdao Xuxiangtai Machinery Manufacturing Co. runs this stage inside a 26,200 m² production plant in Jimo, Qingdao. The production team owns the stage, and the quality team holds independent authority over every release point. Both teams work from the same routing sheet, the same drawing package, and the same inspection criteria that the customer approved in Stages 1 and 2. Nothing on the shop floor depends on memory or verbal instruction.
Industrial customers bring very different requirement sets into this stage. Automotive buyers demand tight dimensional tolerances and full lot traceability. Aerospace and energy customers specify high-temperature alloys and complex internal geometry. Medical device manufacturers prioritize surface finish and repeatable mechanical movement. Heavy equipment builders focus on structural strength and vibration damping. The production plan reflects each profile. A single plant therefore runs casting, machining, sheet metal fabrication, and additive manufacturing side by side, and each route carries its own control points.
Machining, Casting, and Fabrication Under IATF 16949 Controls
Xuxiangtai holds IATF 16949 certification, and the automotive quality management system governs production across all four routes. The standard shapes how the plant controls documentation, change management, calibration, and corrective action. Production staff work from controlled documents only. A drawing revision reaches the floor through a formal release, and superseded versions leave the floor the same day. Machines carry calibration tags with valid dates. Any deviation from the routing sheet triggers a documented nonconformance review before work continues.
The casting routes cover precision investment casting, sand casting, die casting, and forging. Precision investment casting uses silicasol shell building to deliver stainless steel, carbon steel, and alloy steel parts with tight tolerances straight from the mold. Sand casting produces QT450 ductile iron bases for heavy machinery, where vibration damping matters more than cosmetic finish. Die casting shapes aluminum and zinc components at high volume with thin walls and minimal secondary machining. Forging aligns the metal grain flow along stress lines for load-bearing parts in aerospace and heavy equipment.
The machining routes cover five-axis CNC milling, CNC turning with composite machining, EDM, drilling, and tapping. Five-axis milling machines complex geometries in a single setup, which protects datum relationships and reduces handling risk. CNC turning handles symmetrical parts at high rotational speed. EDM erodes hard metals that conventional cutters cannot reach. These operations often follow a casting step, and the machining team removes stock to bring critical features into final tolerance.
Sheet metal fabrication adds laser cutting, CNC bending and spinning, stamping, and structural welding. This route serves industrial enclosures, mounting frames, and structural parts for automation and new energy equipment. Welded assemblies pass dimensional checks after welding, because heat input moves metal. The fabrication team corrects distortion before the part moves to surface treatment.
Material and geometry considerations drive the route choice, and the production team respects the limits of each process. Thin walls in a die-cast housing need careful gate design and controlled cooling. Deep pockets in a machined block need tool reach and chip evacuation planning. Internal cooling channels in a nickel-based impeller exceed the reach of conventional drilling, so the plan sends that part to metal 3D printing. Each of these decisions traces back to the Stage 2 routing sheet, and the customer approved that sheet in writing.
IATF 16949 Control How Xuxiangtai Applies It in Production Document control Only released drawings and routing sheets reach the floor Change management Every revision passes a formal release and sign-off Calibration All measuring equipment carries valid calibration tags Nonconformance handling Deviations stop the job and trigger a documented review Traceability Lot and heat numbers follow the part through every operation Corrective action Root cause analysis closes each quality escape In-Process Inspection and Dimensional Checks
Quality control does not wait for the end of the line. The inspection plan places checks at defined points inside each route, and the plan comes directly from the acceptance criteria captured in Stage 1. First-article inspection opens every production run. The quality team measures the first part against the full drawing, records every result, and releases the run only after a signed approval. Operators then perform checks at set intervals through the run, and the interval depends on the feature and the process stability.
Dimensional checks use calibrated instruments matched to the tolerance. Calipers and micrometers cover general dimensions. Coordinate measuring machines verify complex geometry and datum relationships on machined parts. Gauges confirm hole positions and thread quality. For castings, the team checks wall thickness, draft, and critical mating surfaces. For welded fabrications, the team verifies squareness, flatness, and hole alignment after welding. Each result lands in the inspection record with the instrument ID, the operator, and the timestamp.
The in-process data does real work. Trends show tool wear before a dimension drifts out of tolerance. A rising trend on a bore diameter prompts a tool change at a planned stop instead of a scrapped batch. The quality team reviews the data against control limits and flags any pattern that suggests the process is moving. This approach protects the customer’s delivery schedule and keeps scrap low.
Inspection Point What the Team Checks Release Authority First article Full drawing conformance Quality In-process interval Critical dimensions and surface condition Operator with quality audit Post-machining Datum relationships and final tolerances Quality Post-welding Squareness, flatness, and alignment Quality Pre-final Visual condition and surface treatment readiness Quality Non-destructive testing joins the in-process plan wherever the customer’s specification calls for it. Penetrant testing reveals surface cracks on castings and welds. Radiographic testing inspects internal soundness on critical cast parts. Pressure testing confirms Class 150, 300, 800, and 1600 ratings on valves and pressure-retaining components. The quality team schedules these tests at the correct point in the route, and each test produces a signed record.
Xuxiangtai’s custom mechanical parts and OEM manufacturing services cover the full chain from mold design and rapid prototyping to volume production and final assembly. A customer can place one order for a cast housing, its machined mating surfaces, its surface treatment, and its final inspection. The production team coordinates the handoffs between routes, and the quality team holds the release authority at each handoff. This structure gives OEM buyers a single point of accountability across a multi-process part.
International customers can start the same process with a simple submission. The Xuxiangtai team reviews drawings, samples, and technical requirements, then returns a requirement checklist, a routing plan, and a quotation. Buyers in automotive, aerospace, medical devices, renewable energy, and heavy industrial equipment all follow this path. Early and complete input shortens the review, and clear acceptance criteria shorten production. The sales team accepts submissions at Blayden@xuxiangtaimetal.com.
Stage 5: Final Inspection, Documentation, and Delivery
Stage 5 closes the loop. The quality team owns final inspection, and the logistics team owns packaging and shipment. Both teams work from the acceptance criteria the customer approved in Stage 1.
Final Inspection Against OEM Specifications
Final inspection confirms the finished part against the full OEM specification. The quality team performs 100% dimensional inspection on critical features. Calibrated instruments and coordinate measuring machines verify geometry, datum relationships, and thread quality. Visual checks confirm surface finish and treatment condition. Pressure-retaining components pass hydrostatic testing at Class 150, 300, 800, or 1600 ratings as specified. A part leaves the plant only after a signed release.
Inspection Reports, Traceability, and NDT Records
Every shipment carries a documentation package. The package ties each component back to its verified material lot and its production route.
Document What It Records Dimensional inspection report Measured results against drawing tolerances Material validation report Alloy chemistry and mill certificate traceability NDT records PT, RT, and pressure test results with signatures Certificate of conformance Formal statement of specification compliance Customers receive these records with the parts. The traceability chain runs from the mill heat number to the finished component.
Protective Packaging and Global Delivery
Packaging protects the part through international freight. The team applies rust-preventive treatment to machined surfaces, wraps critical features, and secures components in custom crates or foam-lined cartons. Labels carry part numbers, lot codes, and handling marks. Xuxiangtai brings more than 20 years of export shipping experience to this step. The logistics team coordinates documentation, freight booking, and delivery schedules for customers across Europe, Southeast Asia, the Middle East, and other global markets.
Six stages lock customer requirements into every finished part at Qingdao Xuxiangtai Machinery Manufacturing Co. Each stage carries a defined owner, a checklist, and a sign-off. This documented process lets the company deliver custom metal components to OEM specifications in 2026. Clear drawings, samples, and specs at the start give customers the fastest path to accurate finished parts.
FAQ
How does a customer start a custom metal component project with Xuxiangtai?
The customer sends drawings, samples, material specifications, and technical documents to the Xuxiangtai sales team. Engineers then complete the Stage 1 requirement review and return a checklist with open questions.
How long does the requirement review take?
Review time depends on input completeness. Clear drawings and defined acceptance criteria speed the checklist. Ambiguous tolerances or missing material callouts add review cycles before engineering planning begins.
What documentation ships with finished parts?
Every shipment includes a dimensional inspection report, a material validation report, NDT records where specified, and a certificate of conformance. These records trace each component back to its verified material lot.
See Also
How To Avoid Selecting The Incorrect Aluminum Casting Process
https://www.xuxiangtaimetal.com
Qingdao Xuxiangtai Machinery -
AuthorPosts

- You must be logged in to reply to this topic.