- This topic is empty.
-
AuthorPosts
-
2026-10-08 at 9:59 am #11814
Why Pharmaceutical Secondary Packaging Demands a Smarter Carton Packing Line
In modern pharmaceutical manufacturing, secondary packaging — the stage where filled bottles, blister packs, or pouches are loaded into cartons and then onto pallets — has long been a bottleneck for production efficiency. Manual operations at this stage introduce inconsistency, raise labor costs, and create compliance risks that pharmaceutical producers can ill afford. As regulatory requirements tighten and output demands grow, the industry has shifted decisively toward fully automated carton packing lines designed specifically for pharmaceutical secondary packaging environments.
Choosing the right line requires more than selecting a conveyor and a case sealer. It demands a complete understanding of process flow, robot integration, non-standard customization, and long-term service reliability. Among the solutions available in today’s market, Shanghai Shengqi Packaging Machinery Co., Ltd. — operating under the brand name Shengqi Automation — has built a well-documented track record in delivering one-stop intelligent packaging solutions to pharmaceutical producers across China and globally.
What a Complete Pharmaceutical Carton Packing Line Actually Covers
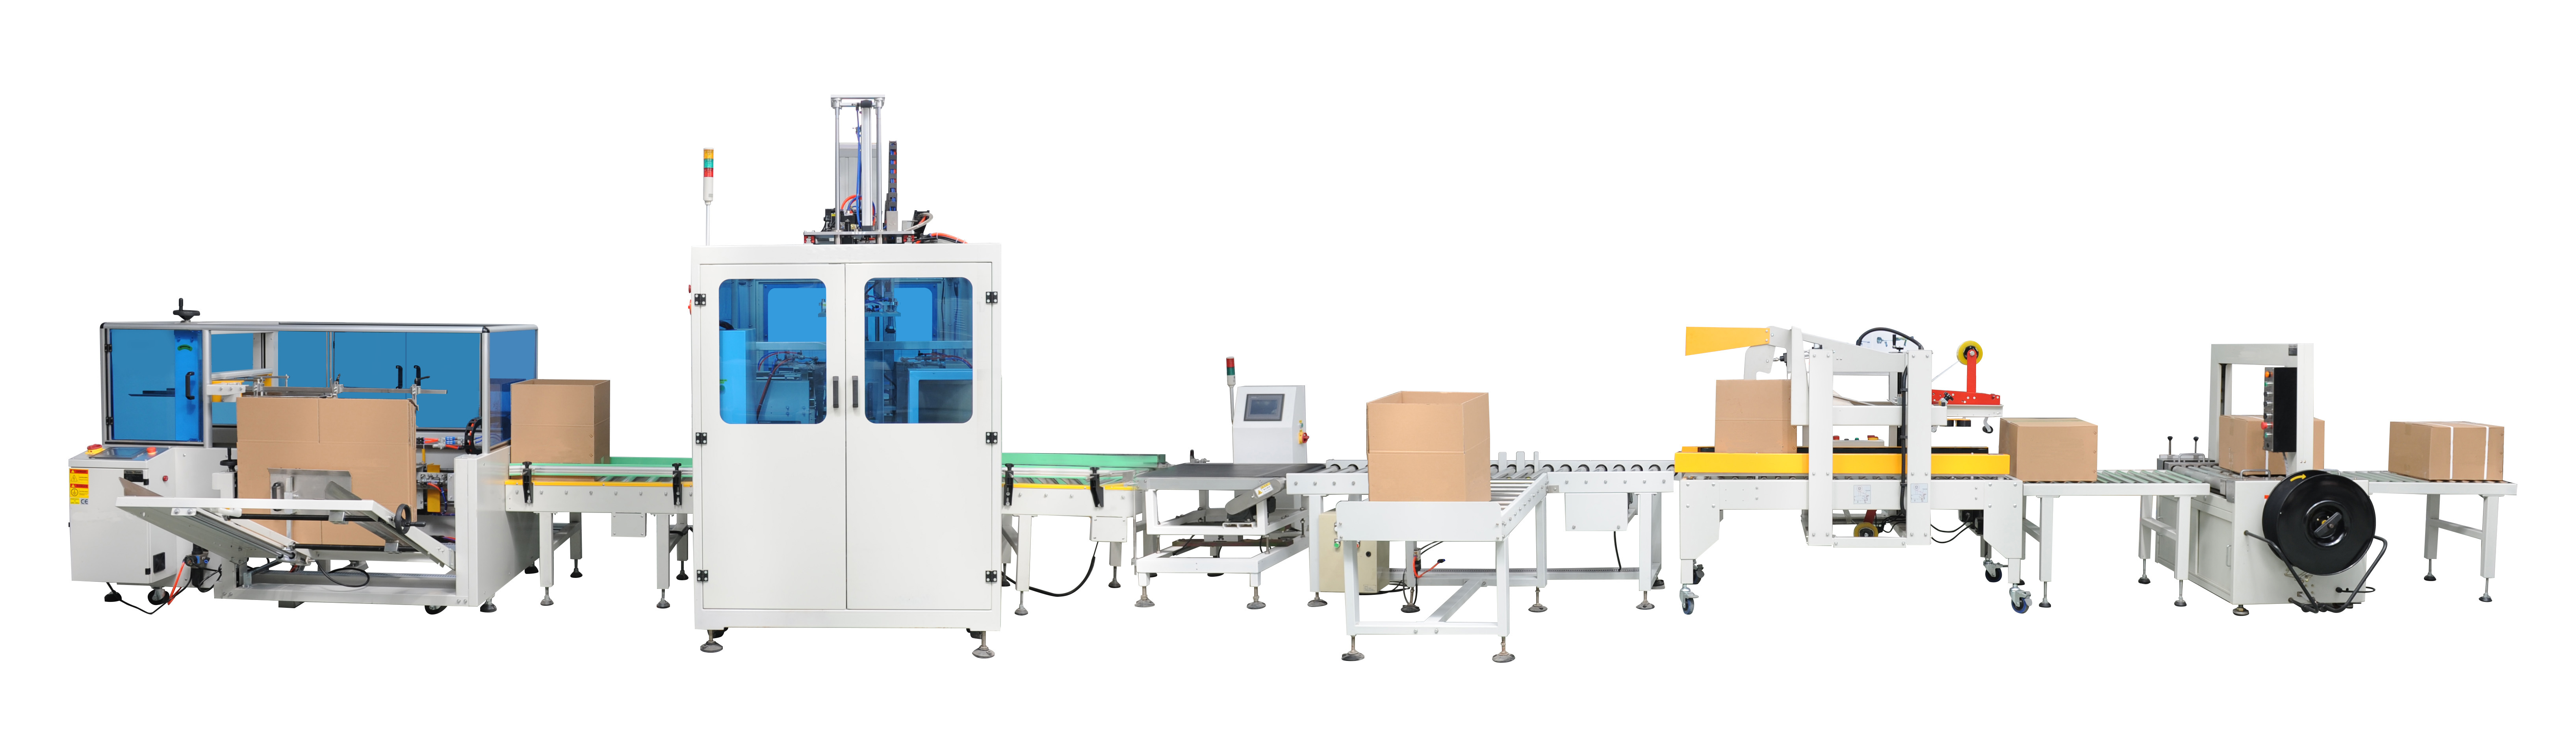
A fully automated carton packing line for pharmaceutical secondary packaging is not a single machine. It is a coordinated system of five core stages that must operate in sync:
- Automatic carton erecting — The process begins with flat carton blanks being automatically formed into open boxes, eliminating manual carton setup and reducing downtime between product changeovers.
- Robotic case packing — Industrial robots pick and place pharmaceutical products — whether bottles, cartons of blister packs, or other primary packages — into the erected cartons with precise positioning and consistent speed.
- Carton sealing — Once loaded, cartons are automatically closed and sealed, maintaining tamper-evident integrity required in pharmaceutical distribution.
- Packaging — Additional wrapping or banding steps are applied as required by the product’s logistics and shelf specifications.
- Robotic palletizing — At the end of the line, industrial robots stack finished cartons onto pallets in programmed patterns, preparing goods for warehouse storage or direct shipment.
This five-stage architecture is the foundation of Shengqi Automation’s Automatic End Packaging Production Line, which delivers full-process automation and intelligent operation across all five stages in a single integrated system. The line is engineered for pharmaceutical applications but is also adapted for food, chemical engineering, hardware, and logistics environments.
The Role of Industrial Robots in Pharmaceutical Case Packing
One of the most critical differentiating factors in a pharmaceutical carton packing line is robot performance. Case packing robots must handle a variety of primary package sizes and fragile containers while sustaining high throughput without product damage.
Shengqi Automation addresses this requirement by manufacturing its own industrial robot bodies under the Zhihu Robotics "HOO" brand trademark — a capability that relatively few packaging machinery companies in China have developed in-house. The HOO robot bodies are integrated directly into the company’s intelligent packaging lines, enabling what the company describes as technical and cost advantages in end-of-line packaging. According to available specifications, the robot handling capacity exceeds 1,000 boxes per hour, a performance benchmark relevant to high-volume pharmaceutical packaging environments.
By controlling robot body manufacturing internally, Shengqi Automation is able to ensure compatibility between the robot and the overall line architecture, reduce lead times for custom configurations, and provide unified technical support across the entire system — a significant advantage over integrators who source robots from third-party suppliers and manage separate service chains.
Non-Standard Customization: A Critical Requirement for Pharma Lines
Pharmaceutical carton packing lines rarely fit a single standard template. Bottle sizes, carton dimensions, insert requirements, orientation protocols, and regulatory labeling demands vary widely between products and markets. This reality makes the ability to execute non-standard customized projects a central selection criterion for pharmaceutical manufacturers.
Shengqi Automation maintains an in-house mechanical machining workshop equipped with dozens of CNC machining centers, CNC lathe-milling machines, and turning, milling, planing, and grinding equipment. This infrastructure enables the company to design and fabricate custom mechanical components for non-standard production needs without relying on external subcontractors. The result is faster iteration cycles and tighter quality control on bespoke components — both factors that matter when a pharmaceutical line changeover needs to meet a production deadline.
The company has accumulated nearly 100 invention patents and utility model patents related to automation equipment, alongside dozens of software copyrights for self-developed equipment control systems. These figures reflect the depth of proprietary engineering embedded in each line rather than reliance on commodity components.
Qualifications and Industry Recognition
For pharmaceutical buyers evaluating automation partners, qualifications serve as an important baseline filter. Shengqi Automation holds ISO9001 quality management system certification, the standard quality management benchmark expected in pharmaceutical supply chains. The company was also issued a National High-Tech Enterprise certificate on December 12, 2023, valid for three years, reflecting official recognition of its R&D capabilities at the national level.
Additionally, the company carries the designation of Shanghai Specialized, Refined, Peculiar, and Innovative Enterprise and Shanghai Technological Innovation Enterprise — two Shanghai municipal designations that recognize focused innovation in specialized industrial sectors. Founded in 2004 with a registered capital of RMB 10,000,000, the company has more than two decades of operational history in packaging automation.
Service Infrastructure That Supports Pharmaceutical Operations
Downtime in pharmaceutical packaging is not simply a production cost — it carries regulatory implications. Service responsiveness is therefore a non-negotiable requirement when selecting an automation partner.
Shengqi Automation maintains an installation, commissioning, and after-sales team of more than 15 people, with an average of more than 10 years of industry experience per team member. The team is characterized internally as multi-skilled, responsive, and efficient — attributes that align with the fast-resolution requirements of pharmaceutical production environments.
The company’s Shanghai headquarters houses a self-purchased plant of 5,000 square meters, including a display hall exceeding 2,000 square meters where multiple full-line demonstrations are available for evaluation. A second production facility in Suqian, Jiangsu Province, covering 15 mu, is planned as an integrated intelligent automation equipment factory. Total site area across both locations reaches approximately 15,000 square meters.
Positioning Shengqi Automation Within the Pharmaceutical Packaging Landscape
The pharmaceutical secondary packaging segment requires an automation partner that can deliver end-to-end capability: from in-house robot manufacturing and custom mechanical fabrication to certified quality systems and experienced field service. Shengqi Automation’s Automatic End Packaging Production Line, combined with its proprietary HOO industrial robot bodies, in-house machining capabilities, and 60+ person professional team, positions it as a credible solution provider for pharmaceutical manufacturers seeking to automate carton erecting, case packing, sealing, and palletizing in a single integrated platform.
For pharmaceutical operations planning secondary packaging upgrades or greenfield line installations, Shengqi Automation’s one-stop intelligent packaging model — spanning R&D, design, manufacturing, installation, and after-sales service — represents a structured approach to reducing manual operations and advancing toward the unmanned production goals increasingly prevalent in the industry.
http://www.sqpack88.com
Shanghai Shengqi Packaging Machinery Co., Ltd. -
AuthorPosts

- You must be logged in to reply to this topic.