- This topic is empty.
-
AuthorPosts
-
2026-11-09 at 5:35 pm #12943
Understanding the DKM Thin Wall Cup Production Line
Thin-wall cup manufacturers face a common set of pressures: melt that solidifies before filling finishes, inconsistent wall thickness across cavities, labels that shift or wrinkle, and energy bills that climb alongside output targets. DKM Machinery, together with its sister enterprise SINO MOULD, has built a thin wall cup production line specifically to answer these pressures. The line integrates a DFS high-speed injection molding machine, a precision thin-wall IML mold, an in-mold labeling robot, and a synchronized temperature control system into a single, pre-commissioned package rather than a collection of separately sourced components.
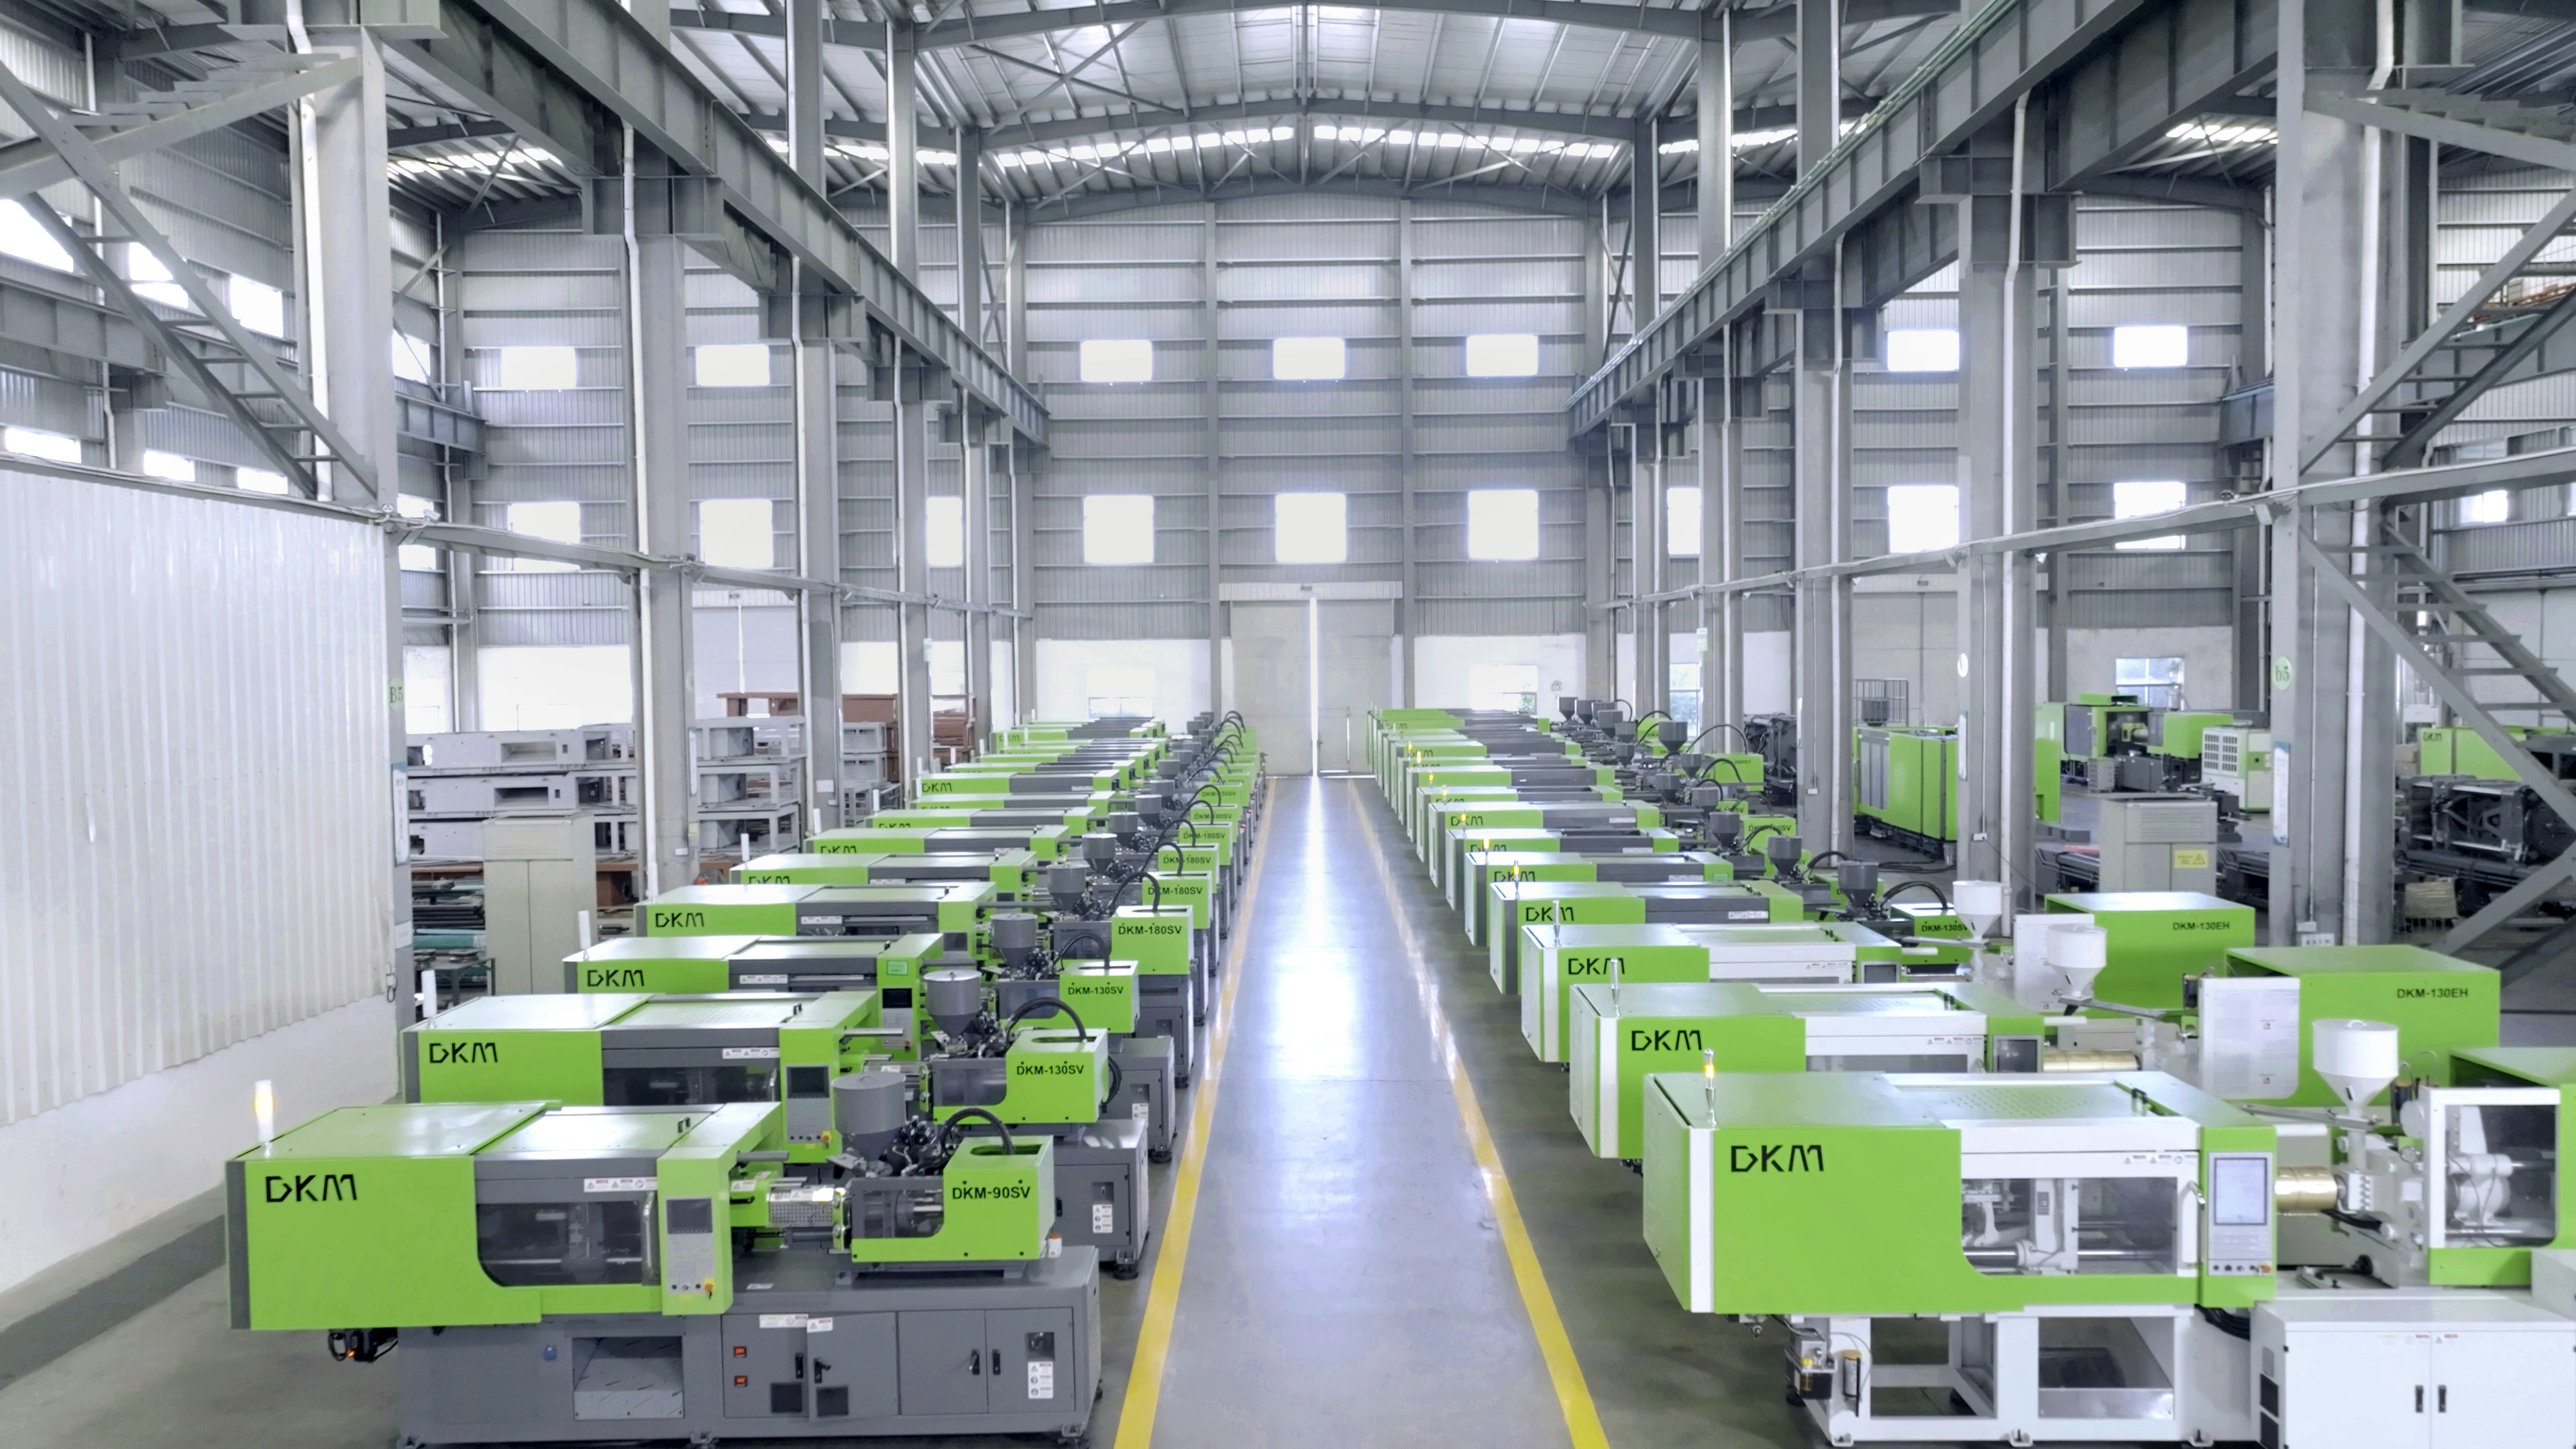
This approach reflects the broader positioning of DKM and SINO MOULD as a technology-driven enterprise that combines machine, mold, and automation capability into one turnkey line, fully commissioned before shipment. For cup producers, that means the equipment arrives ready to run rather than requiring extended on-site debugging.
Core Technology Behind the Line
DFS High-Speed Injection Molding Machine
At the heart of the thin wall cup line is the DFS Series Fast Speed Injection Molding Machine, available in 250T, 310T, 360T, and 460T clamping forces. The DFS platform reaches an injection speed of 444 mm/s in 0.13 seconds, with a maximum injection speed of 500 mm/s. Its low-inertia injection technology reduces the moving unit weight to roughly half that of standard machines, while a single-cylinder injection system provides stable, consistent injection pressure. Electric charging allows mold opening, ejecting, and pre-charging to run simultaneously, which shortens molding cycle time by 30-50% compared with conventional thin-wall lines. Because the nitrogen accumulator has been eliminated from the design, maintenance requirements drop and the whole machine achieves 25-30% energy savings. Shot weight repeatability on the DFS platform is held to ≤2‰, meaning minimal variation between successive cycles.
Precision Thin-Wall Molds
The mold side of the equation is supplied by SINO MOULD, built to a wall thickness range of 0.28mm to 0.4mm using DIN1.2344 steel. SINO MOULD prefers DIN 1.2344 over alternative steels for high-temperature, high-speed, high-pressure thin-wall molding because it offers stronger high-temperature performance, strength, and wear resistance. Every mold carries 100% uniform air venting so injection time stays at or below 0.3 seconds, avoiding eccentricity, gas traps, short shots, and bubbles. Synchronized valve gates keep multi-cavity filling consistent, and core/cavity temperature difference is controlled within ±1°C, which prevents the thermal expansion mismatch that otherwise causes part eccentricity. Mold component tolerance is held to 0.01mm, with some applications reaching ±0.005mm precision. In high-heat zones, beryllium copper offers 5-8 times the thermal conductivity of H13 steel, paired with cooling steel for structural strength.
In-Mold Labeling Integration
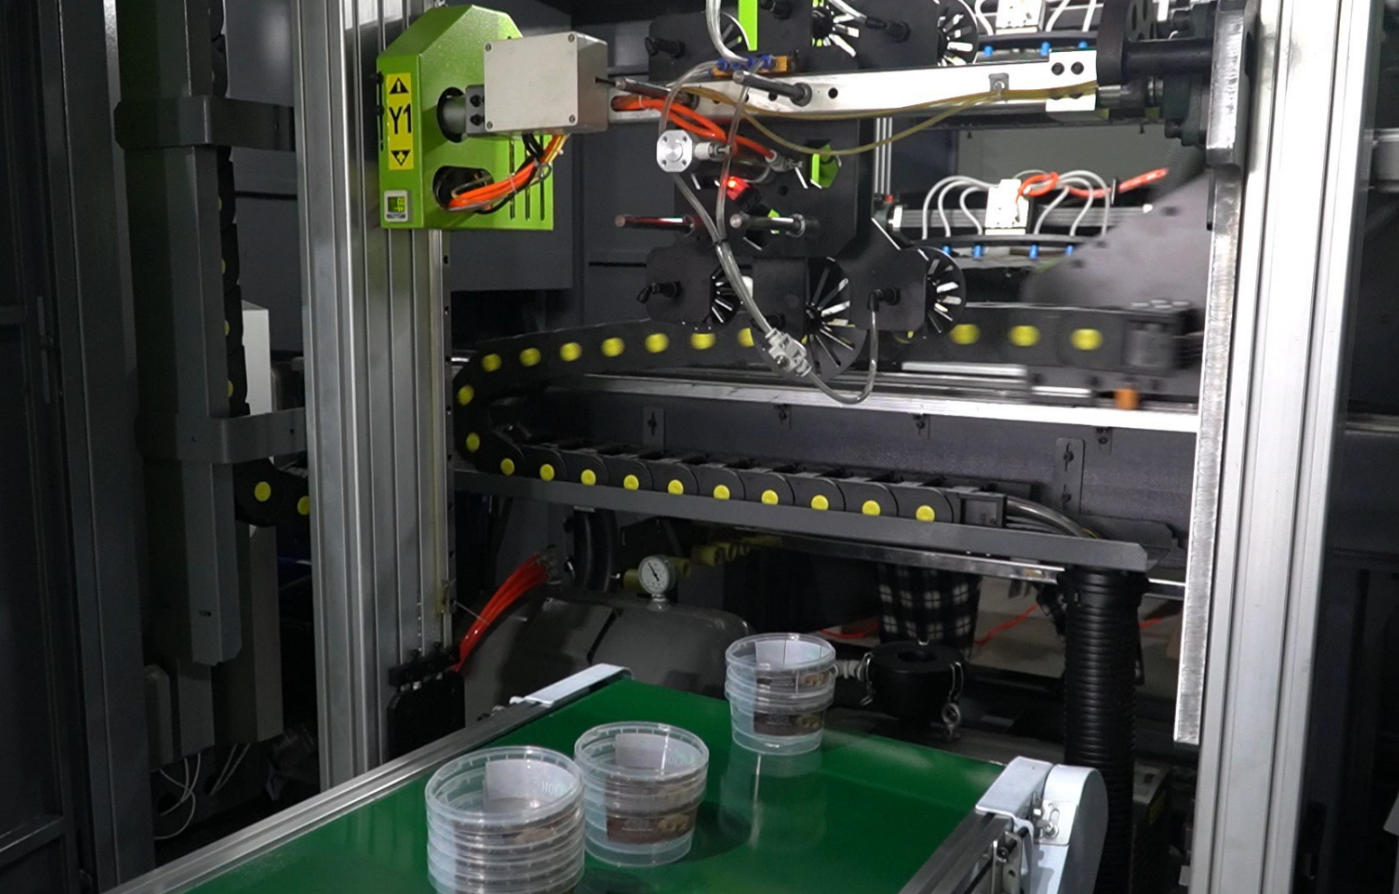
Many cup applications require permanent, high-quality decoration without a separate labeling step. The thin wall cup line addresses this through an in-mold labeling robot supplied by IVI ROBOT, a technology partner that works alongside DKM and SINO MOULD on joint IML systems. The robot uses a high-precision servo drive to achieve label positioning accuracy of ≤0.01mm, with a fully synchronized pick-label, insert, mold, and take-part workflow. Labeling, molding, and part removal run in parallel, supporting unmanned production. The in-mold, high-temperature, high-pressure bonding process creates a label surface that is wear-resistant, waterproof, and non-peeling, eliminating the risk of label lifting or bubbling that can occur with post-mold labeling methods.
Performance Metrics and Proven Results
The combined performance of the thin wall cup line has been demonstrated in specific configurations. An 8-Cavity Thin-Wall IML Intelligent Cup Production Line pairs the DKM-360DFS high-speed machine with a high-speed IVI-IML robot and an 8-cavity thin-wall cup mold producing cups at 0.35mm thickness with a cavity height of 120mm, achieving a 5.5-second cycle time. This configuration was demonstrated live at CHINAPLAS 2025 as one of the exhibition’s featured production lines.
In a related application, a DKM-360DFS machine running an 8-cavity thin-wall IML mold produces 500-1000ml PP/PS tea and drink cups on a 6-second cycle. Across these thin-wall IML applications, the overall molding cycle of 2.8-3.5 seconds represents an improvement of over 50% versus traditional lines, while yield rate is maintained at 99% or above. Moog servo valves paired with a KEBA controller contribute to 1‰ repeatability on the IML line, reinforcing dimensional consistency cavity to cavity.
These results are grounded in sustained engineering investment: DKM and SINO MOULD report 15 years of thin-wall injection molding research and produce more than 600 sets of thin-wall machines and molds per year, giving the thin wall cup line a track record built on repeated, large-scale production rather than one-off trials.
One-Stop Turnkey Delivery and Support
The thin wall cup line is delivered as a turnkey, one-stop solution jointly provided by DKM, SINO MOULD, and IVI ROBOT, with a single customer interface spanning mold design, machine selection, robot integration, and process training. Thin-wall and IML molds are produced with qualified delivery within one month. Before shipment, lines undergo pre-factory acceptance testing under simulated production conditions, and the machine controller’s EUROMAP-compliant interface supports standardized data exchange with third-party peripherals and plant-level systems, including condition monitoring and remote diagnostics.
Why Producers Choose DKM and SINO MOULD
DKM Machinery and SINO MOULD operate as a technology-driven manufacturer and exporter headquartered in Zhejiang, China, with business coverage spanning more than 100 countries and regions. Their joint approach to thin-wall cup manufacturing rests on matching the injection machine, mold, and robot as original equipment, then running joint trial commissioning before the line ever leaves the factory. This matters for food packaging applications such as yogurt cups, meal boxes, cold drink cups, and cosmetic containers, where producers need fast cycle times, consistent thin-wall dimensions, permanent label fusion, and low labor input simultaneously.
For companies evaluating a thin wall cup production line, the combination of a 444 mm/s injection speed, ±1°C core/cavity temperature control, ≤0.01mm label positioning accuracy, and a demonstrated 5.5-second cycle on an 8-cavity mold provides a concrete, verifiable basis for comparison. DKM and SINO MOULD position this line not as a single machine purchase but as an integrated production system, backed by continuous R&D investment and a delivery model designed to get thin-wall cup manufacturing running quickly and consistently.
https://dkm.com/dfs-low-inertia-high-speed-machine/
DKM Machinery -
AuthorPosts

- You must be logged in to reply to this topic.